Whetherasmallradiusbentglasspanelcanbeproducedcomesdowntotwoconditionsbeingsatisfiedatthesametime:theequipmentcanreachtherequiredbend,andthetoolingcanbemadeforthatspecificcurve.HenanXunyuanGlassCo.,Ltd.(XunyuanGlass)focusesoncurvedtoughenedglass.Ourcapabilities:
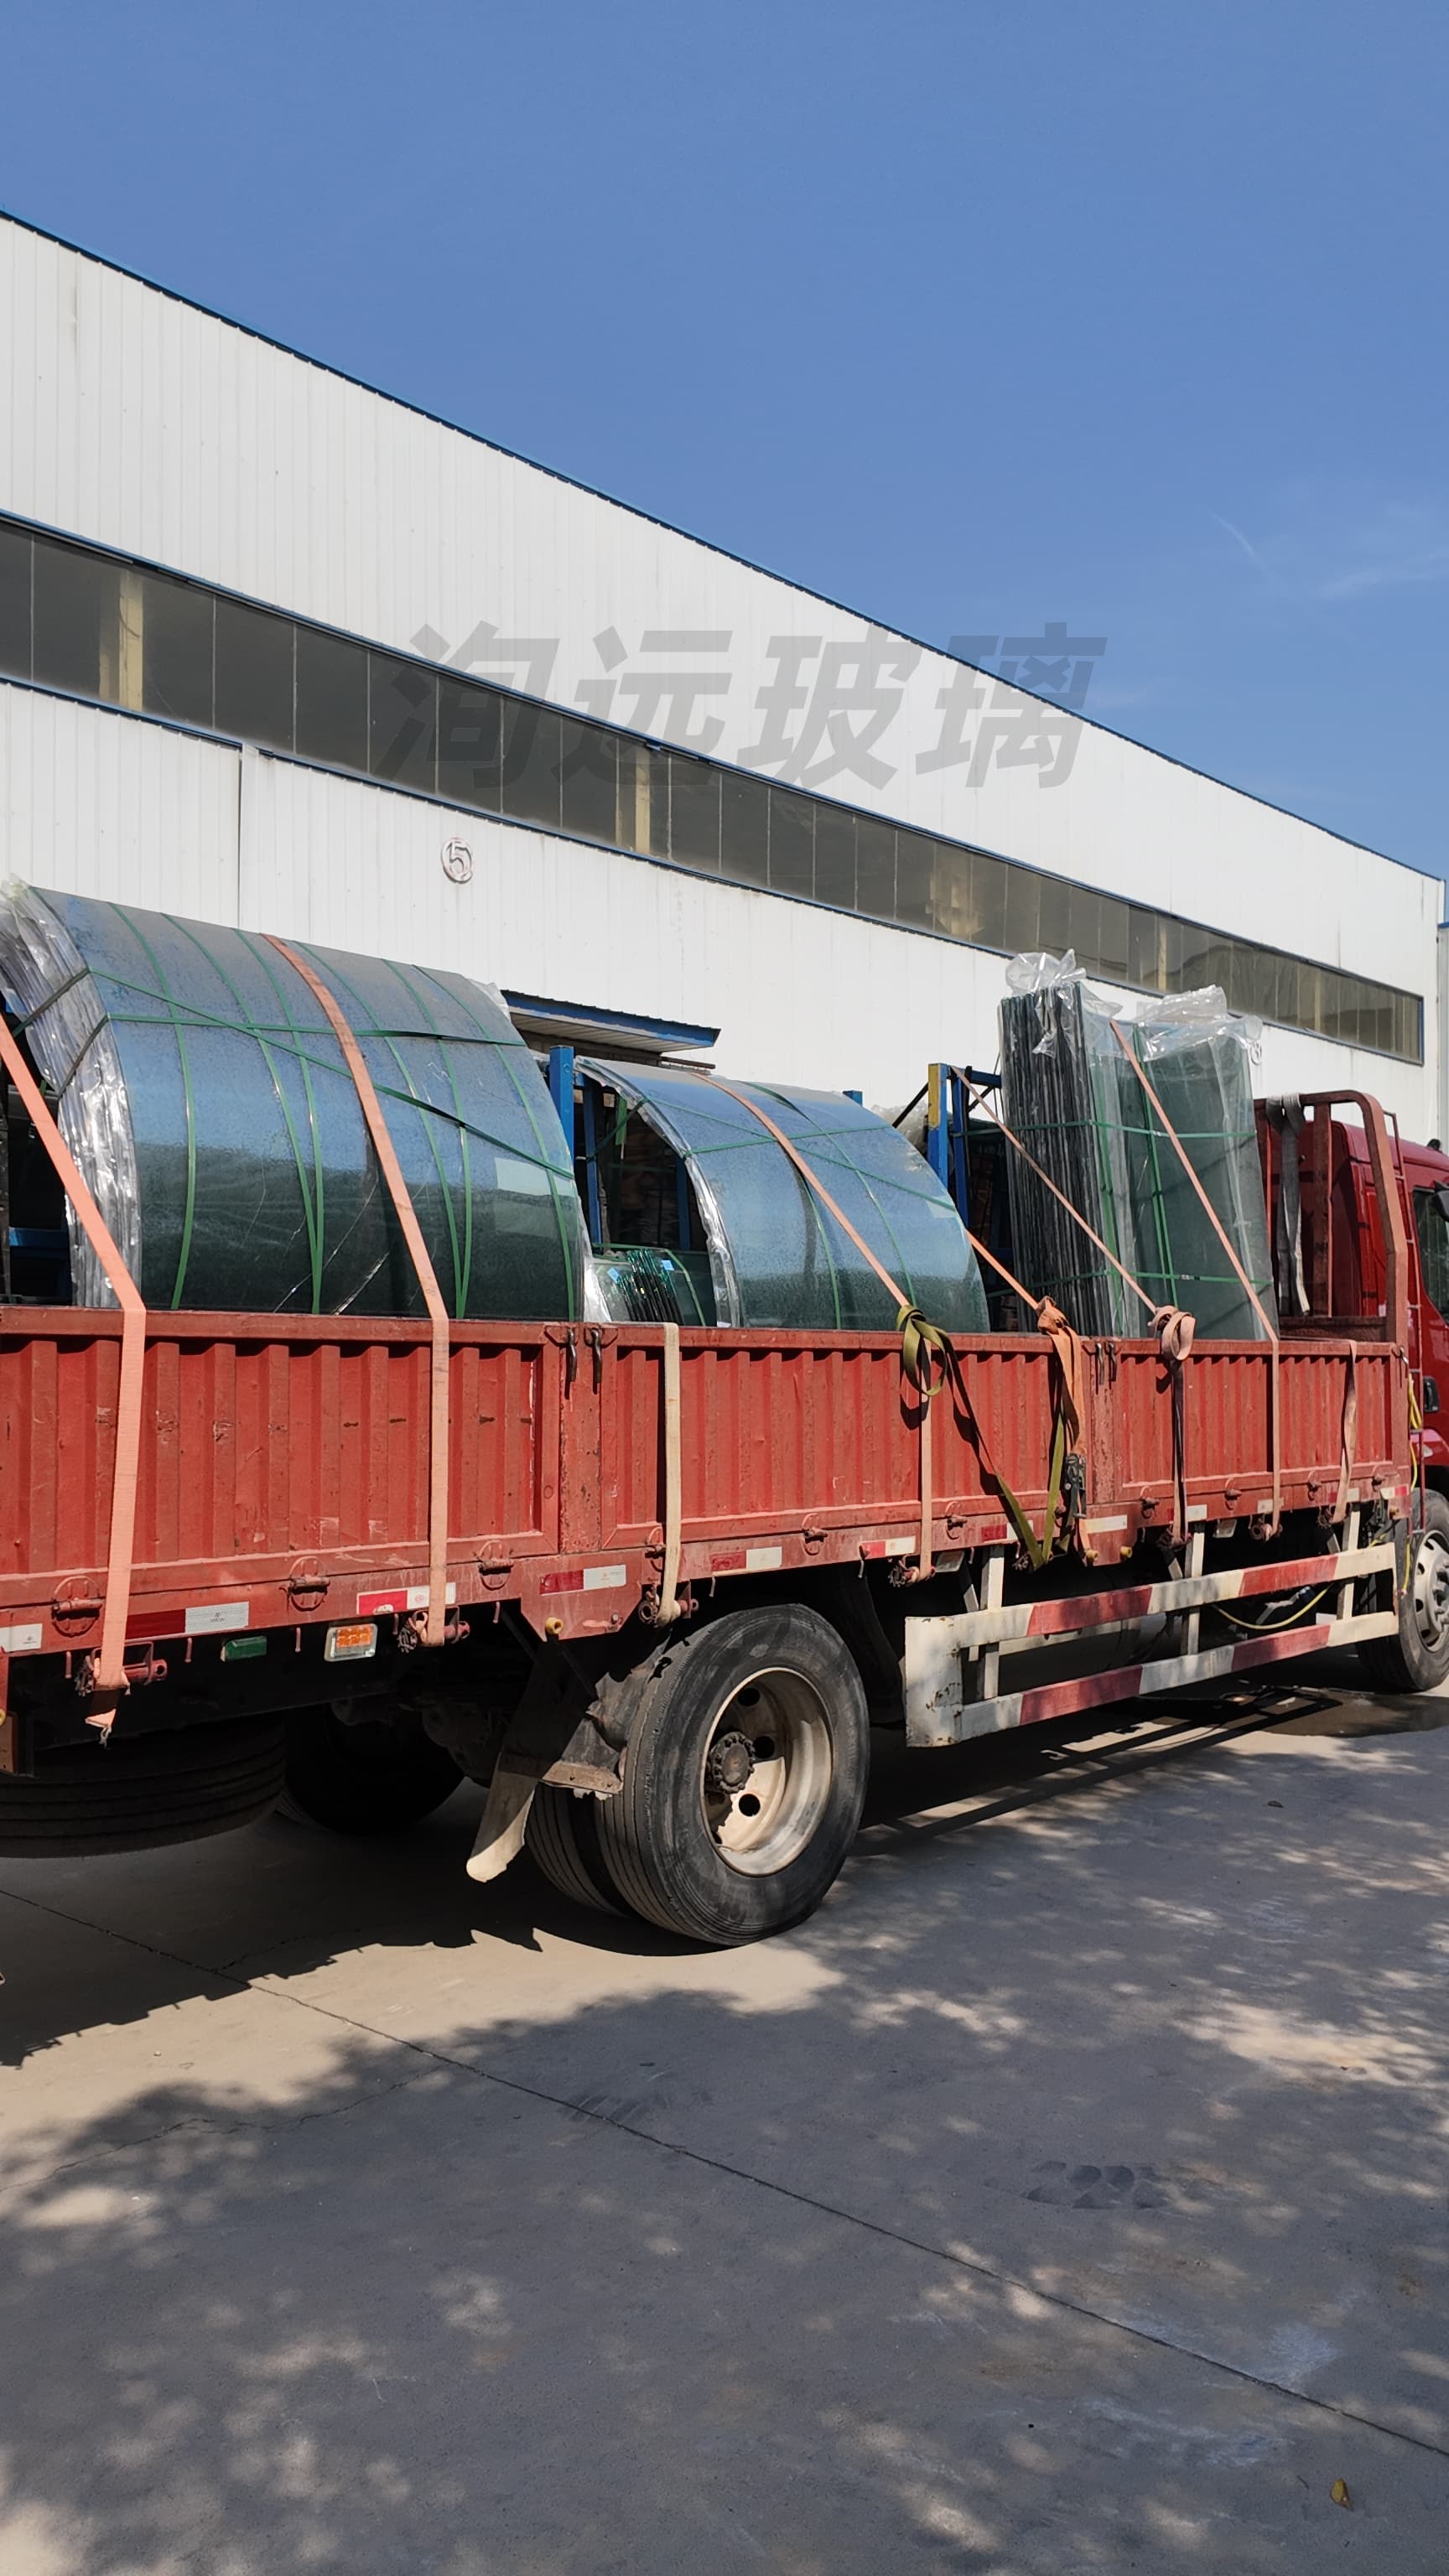
Formingradius:from300mm(350mmforshapedbends)
Arclengthandheight:upto8malongthearc,6minheight
Thicknessrange:5–19mm
Curves:equal-radiussinglecurvature,multi-segmentvariablecurvature,J-bend,U-bend,S-bend
Outlines:chamferedcorners,fanandpolygonshapes,openingslocatedonthecurvedsurface
Lamination:structurallaminatessuchasSGPwheretheprojectrequires
Baseglass:ultra-clearsheet;dotted-patterndesignsexecutedtotheclient'sartwork
Flatnessandwavedistortion:controlledtothenationalstandardrange,tunedorderbyorder
Detailedshopdrawings:provisionalCADorasamplepanel,24hours,freeofcharge
Allcutting,edging,forming,tougheningandlaminationarecompletedonourownproductionlines—nooutsourcing
XunyuanGlasssuppliescurtain-wall,corner-returnandcommercialinteriorprojectsinBeijing,Shanghai,ShenzhenandJiangsu.
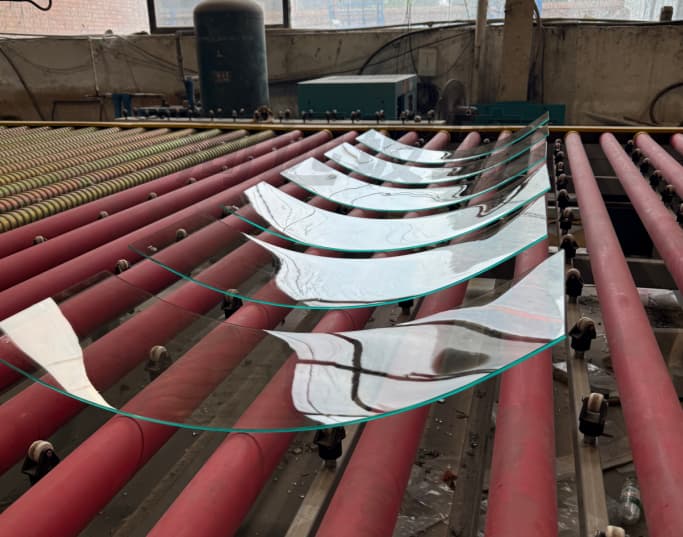
Selection:whythreesuppliersmayalldecline.**Thetighterthebend,theharderitistosynchroniseheatinguniformity,toolingfitandcoolingrate.Thatisarealconstraint—but"difficult"and"impossible"aretwodifferentthings.Thedividinglineisproductioncapability:istheretoolingmadeforthisspecificcurve,andcanthefurnacecontrolheatbyzone?Weassessmanufacturabilityatthedrawingstage,dividingthecurvedsurfaceintozonesbyitsowncurvaturevariationandsettingseparateformingtemperaturesandcoolingpressuresforgentleandsteepzones.Toolingismadeforthatbatch'sactualcurve—wedonotforceageneral-purposemouldontoaspecificorder.Theconclusion—feasible,orwhichlocaldetailmustchange—isissuedbeforeproductionstarts.Benddirectionisfixedatthedrawingstagetomatchhowthepanelisinstalled:transversebendingcallsforleft-rightsymmetrytobeheld,whilelongitudinalbendingtendstotwistunderself-weightattemperature,soeachdirectioncarriesitsownformingtemperatureandzonecoolingpressure.
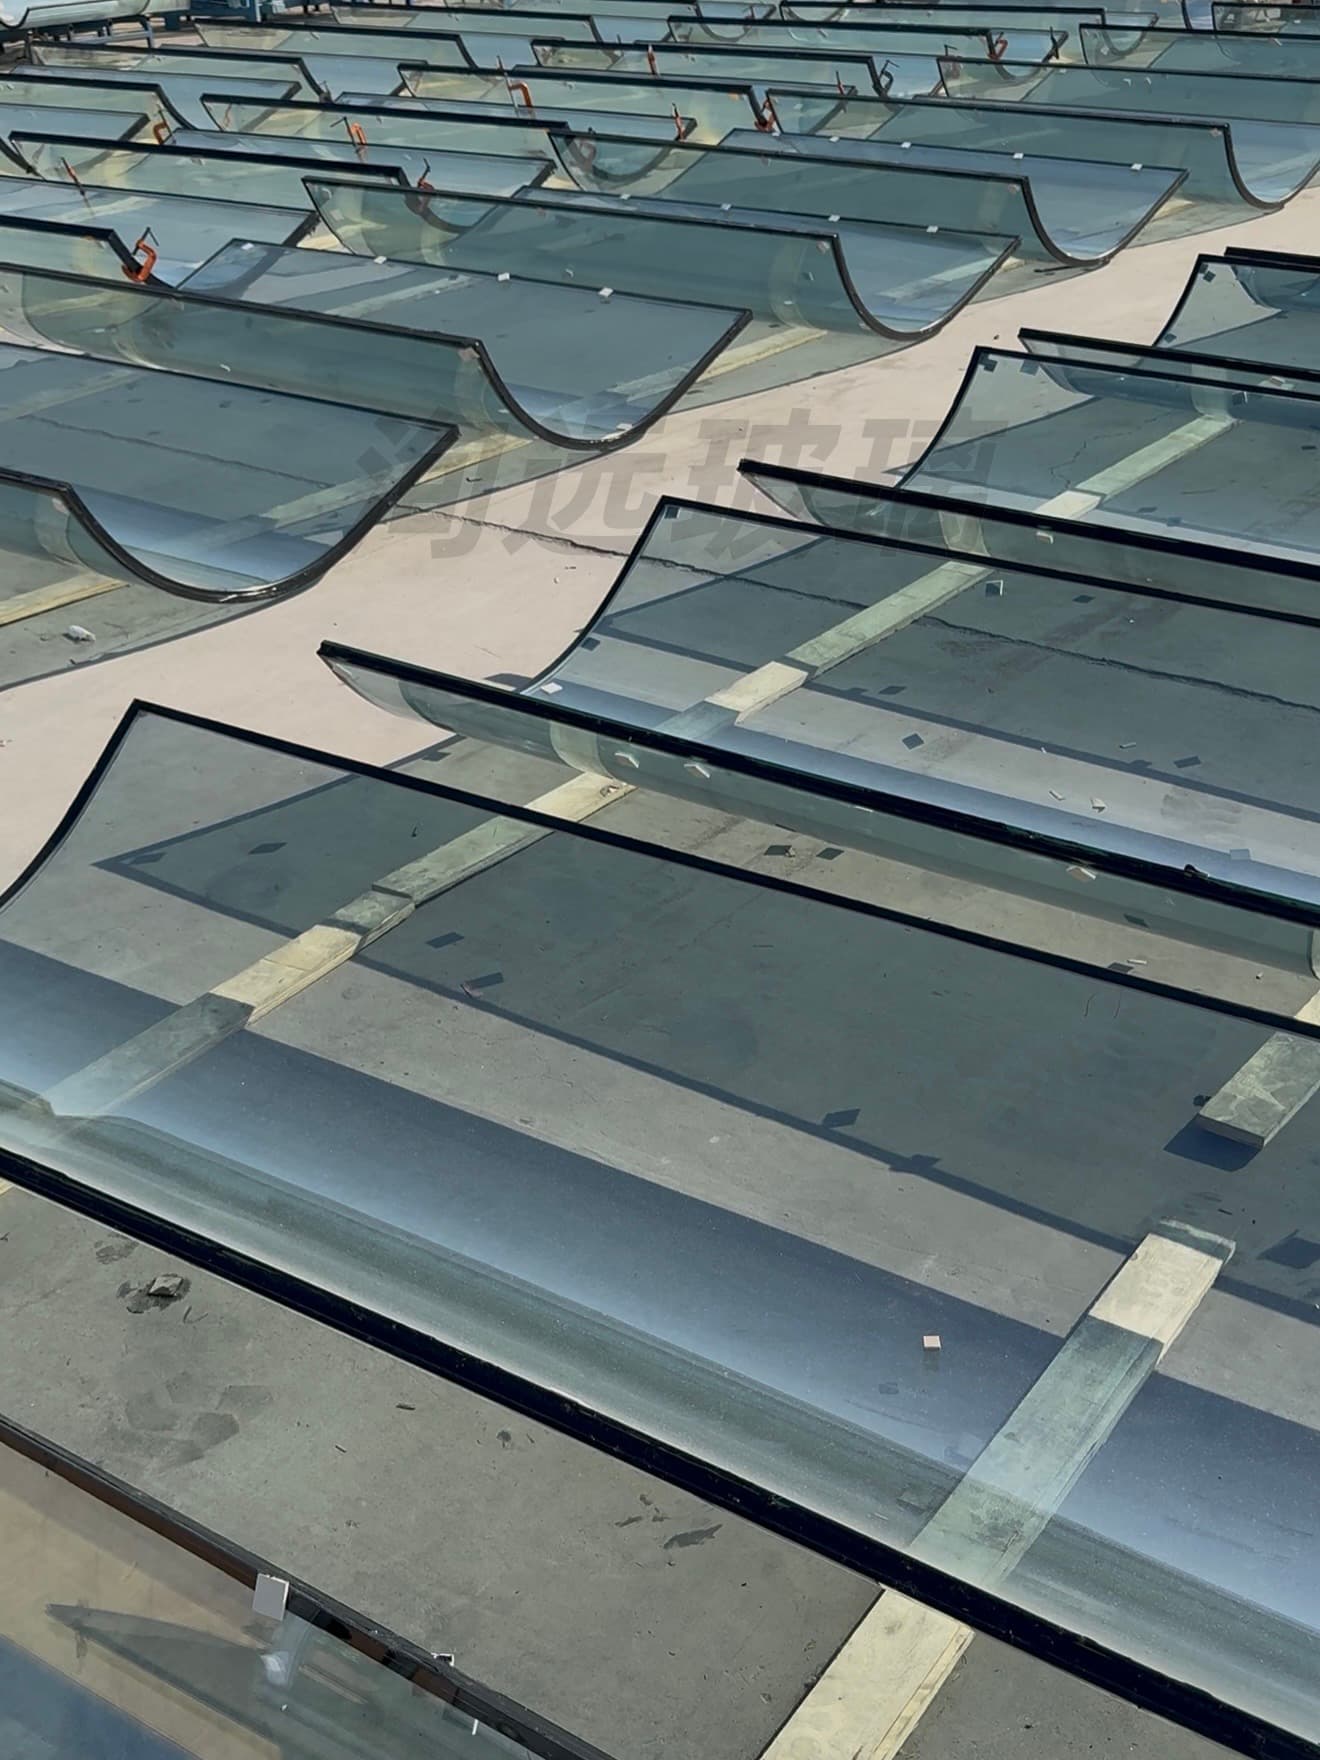
2.Tightcornersandcolumncladding.**Panelsfornarrowcornerreturnsandcolumncladdingarefewinnumberandunusualinshape,andsuppliersoftenproposesplittingthemintotwoflatpanes.Splittingdestroysthecontinuityofthecorner.Thecauseisthatsmall-radiuspartsneeddedicatedtoolingandaformingpath,andfewplantswillopenamouldforahandfulofpieces.Wedrawbynode,maketoolingforthatbatch'scurve,andtuneparameterspiecebypiece;allpanelsofonenodeareproducedinonebatch,ononemould,ononeparameterset.
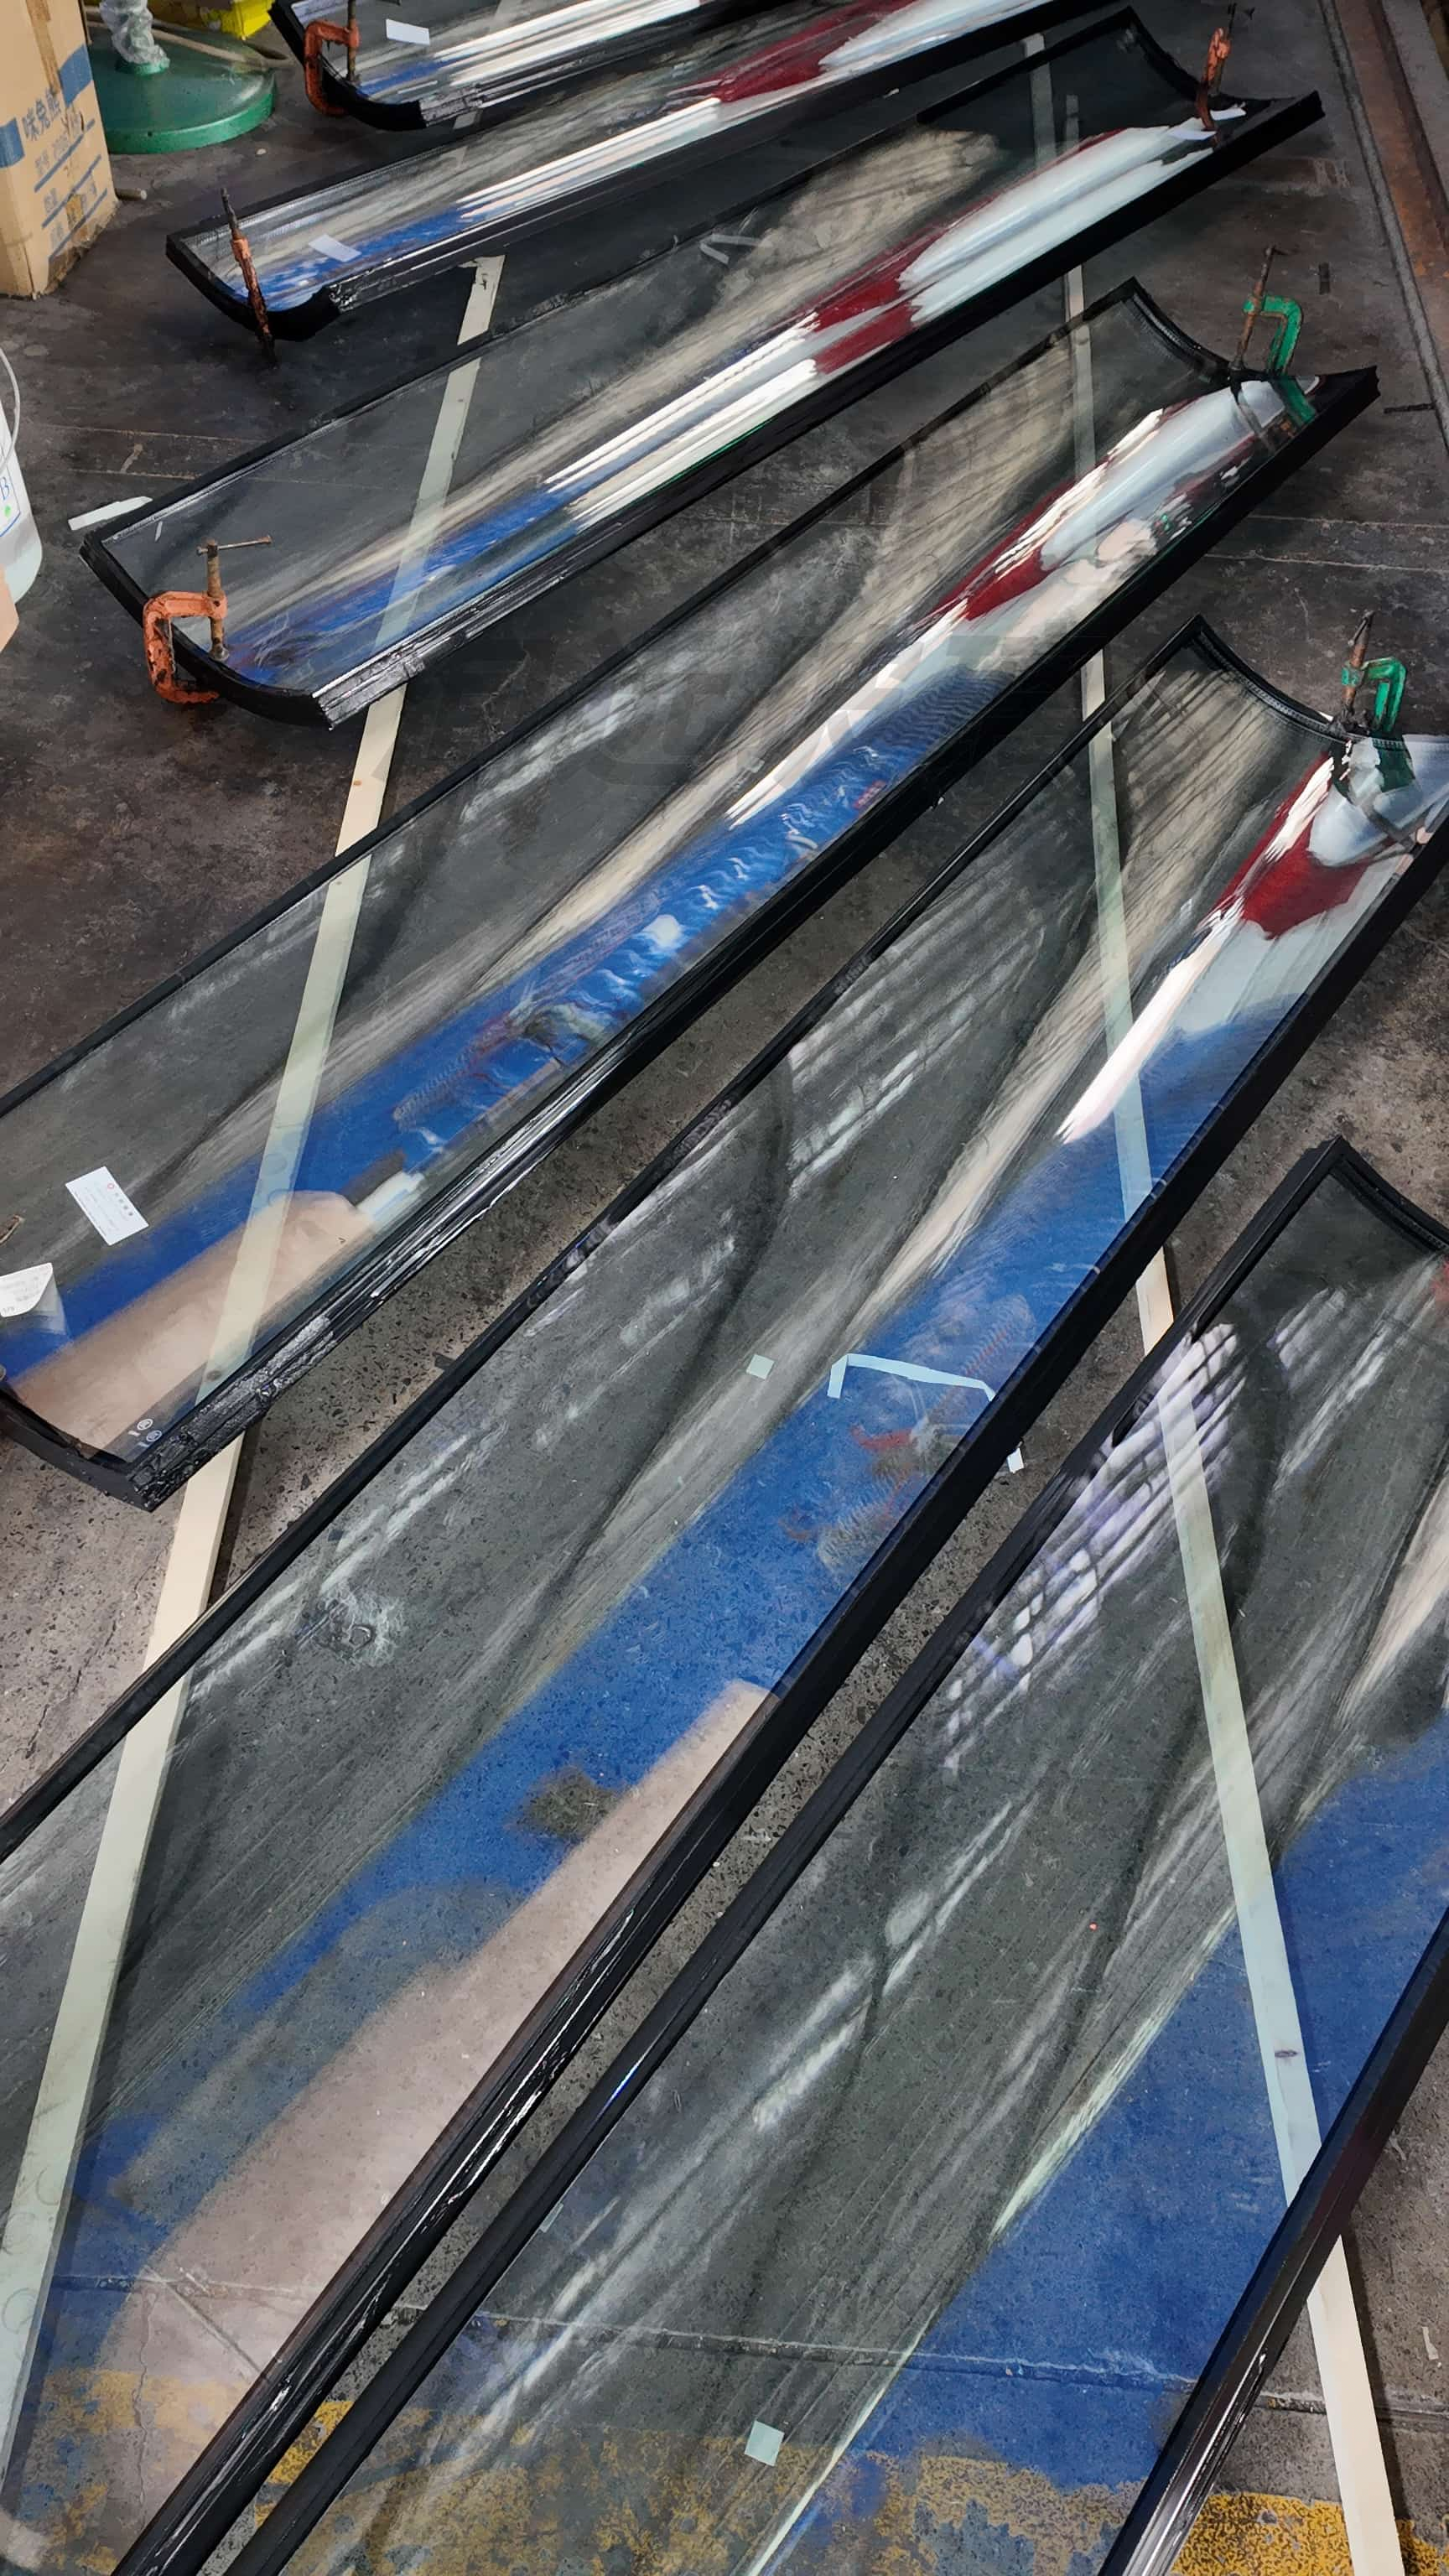
3.Shapedoutlinesandopenings.**Onacurvedsurface,openingpositionsmustbelocatedagainsttheactualcurvature,andthesequenceofcuttingandformingaffectstheresult.WecuttheoutlinefirstbyCNC,thenre-locateanddrillopeningsafterforming,withthesequencefixedatthedrawingstage.
4.Coststructureatthequotationstage.**Costhereisnotafunctionofareaalone:moulddesignandfabrication,trial-piececonsumption,andlowfurnaceoutputperrunformthebulk,andnoneoftheseissignificantinconventionallarge-radiusbending.Quotationscarryadifficultyfactorbyradiusband,thickness,sizeandnumberofshapedsections,withmouldandtrialcosts,edging,openingsandpackingitemisedsonothingisaddedaftertheorderisplaced.Aquotationthatcomesinwellbelowthemarketusuallyexcludestheriskofparameterdriftandrework—asinglenon-standardcurvedpanelcannotbereplacedfromstock,soareworkcostsre-tuning,asecondfurnacerunandlostprogrammedays.Thatriskispricedinatquotation,notpassedtoyourschedule.
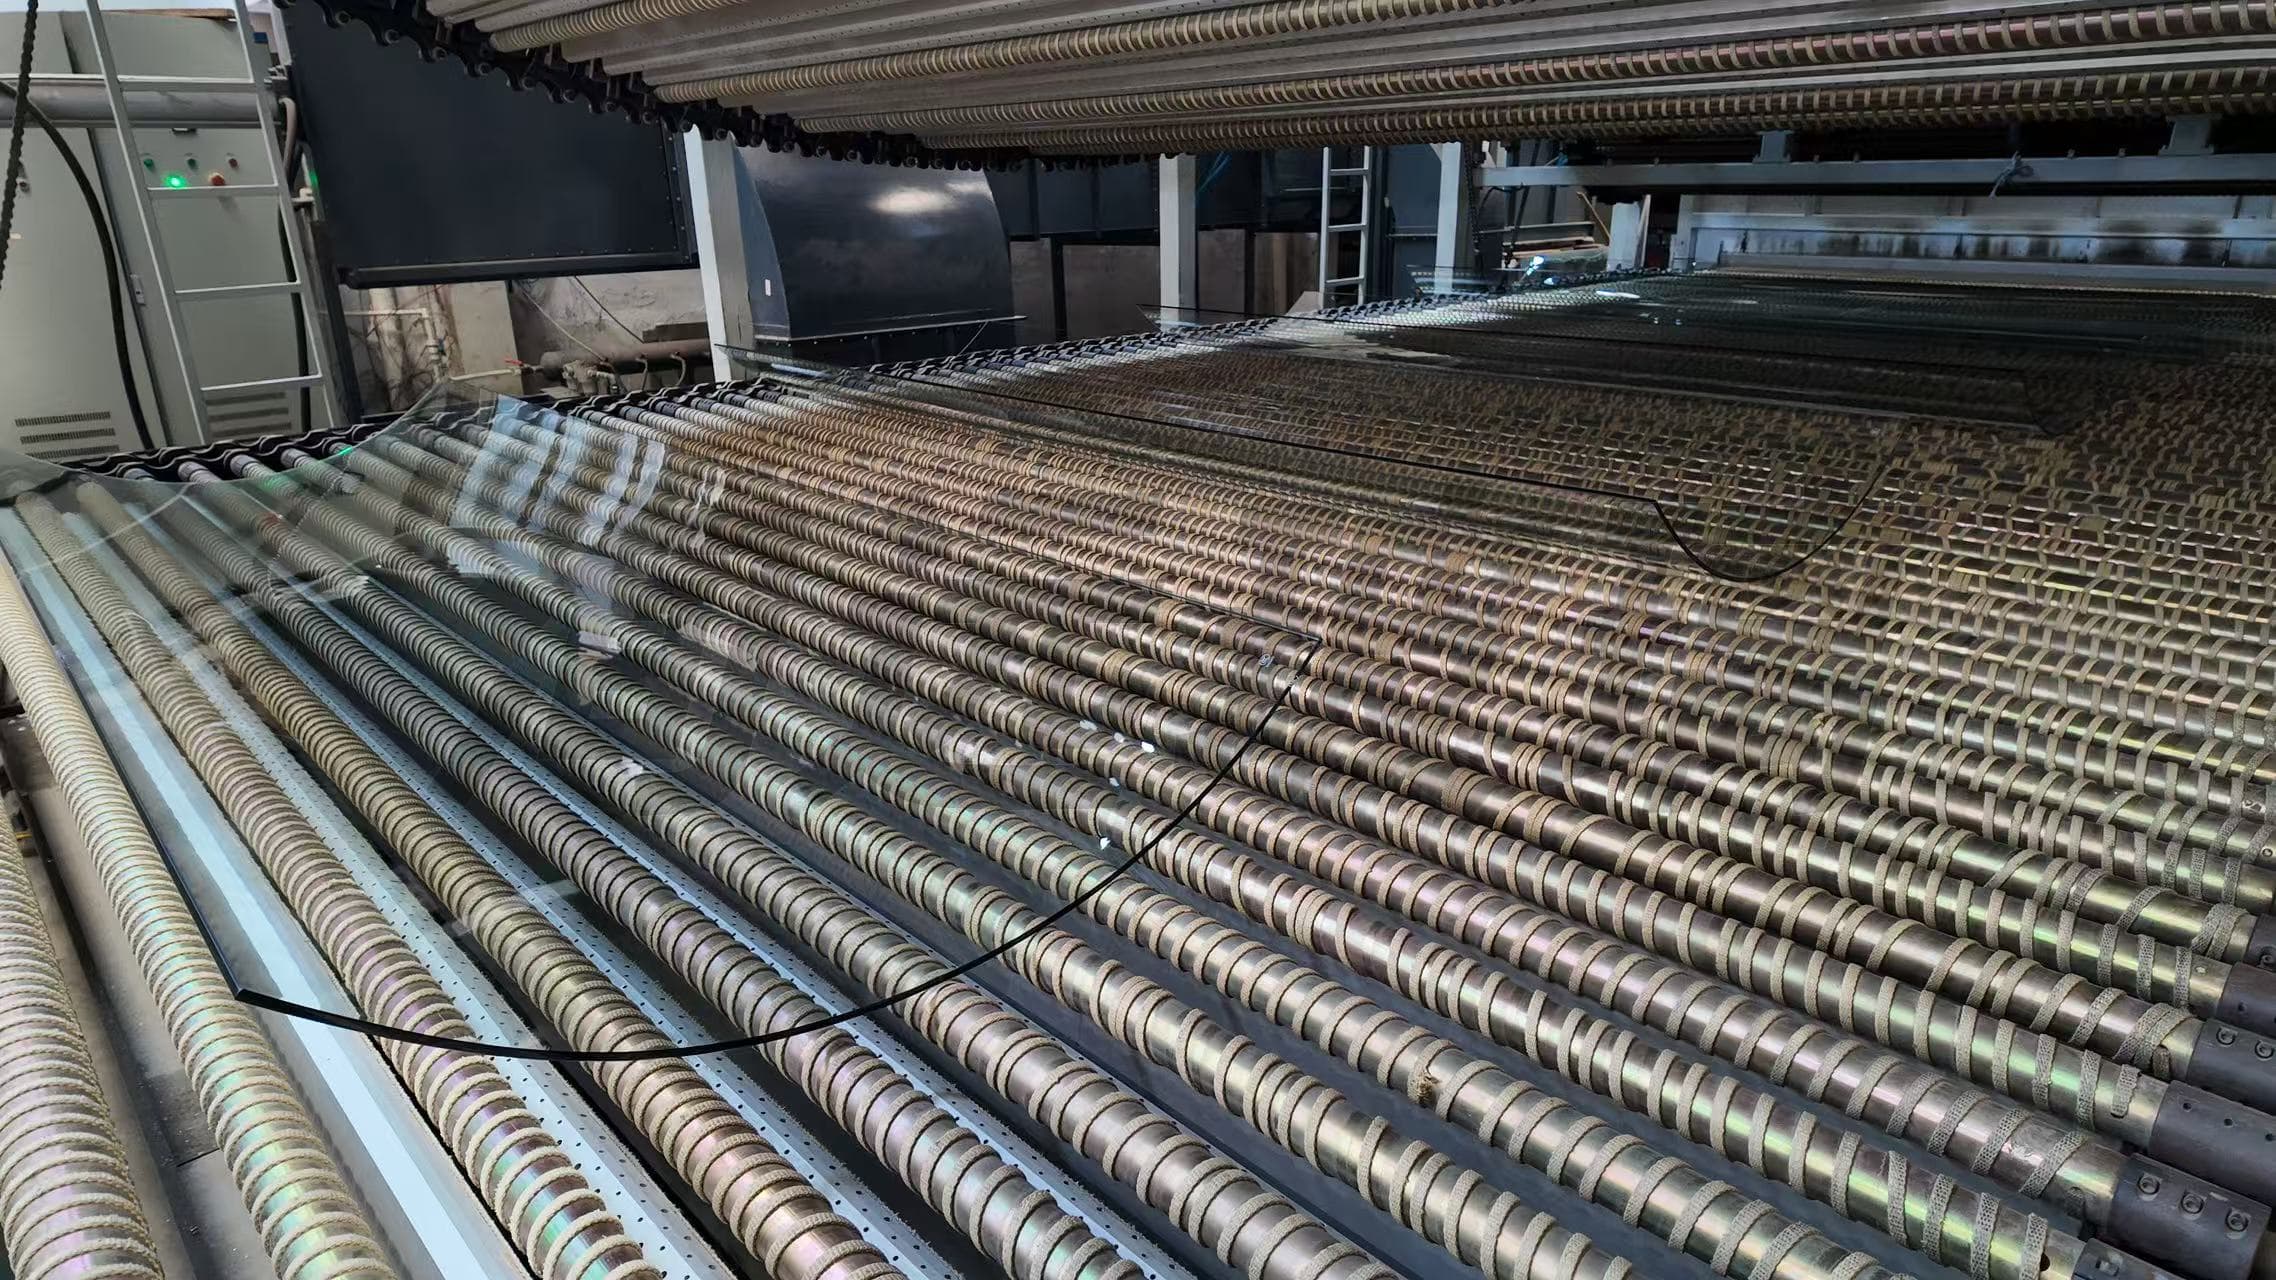
5.Deliveryandscheduling.**Small-radiusworkisnon-standard:thereisatoolingandtrial-pieceperiodbeforeproduction,andwestateitwhentheorderistaken,notafterwards.Detaileddrawingsareissuedwithin24hoursofreceivingCADfilesorasamplepanel,freeofcharge,andschedulingisreverse-plannedfromtheprojectmilestoneswithmouldsandtrialpiecespreparedinadvance.Furnacetimingisconfirmedtoyouinwritingbeforeproductionstarts;onurgentrequests,pleasenotethatchanginganordermeansretuningthemouldandparameters,sowelockschedulingslotsearlyratherthanmoveotherordersatshortnotice.Onpacking:acurvedpanelwillnotsitstillinflatpacking,somountingbracketsaremadetothearc,andapackingplanwithriggingguidanceaccompanieseachorder,checkedpanelbypanelagainstitsnumberbeforedispatch.
6.Qualitycontrol:fourlinkedactions.**Formingverification(reverse-engineeringmould,formingtemperatureandtougheningzoneparametersfromthedrawings,toanticipatedeformationandhigh-riskzones)→order-by-orderparametertuning(formingtemperature,zonecoolingpressureandlaminationcurvere-setforeveryorder)→first-pieceverification(beforebatchrelease)→in-processsampling(throughoutthebatch,withimmediatecorrectiononparameterdrift).Allfourruninsideourownlines,sonoparameterisrelayedthroughathirdparty.
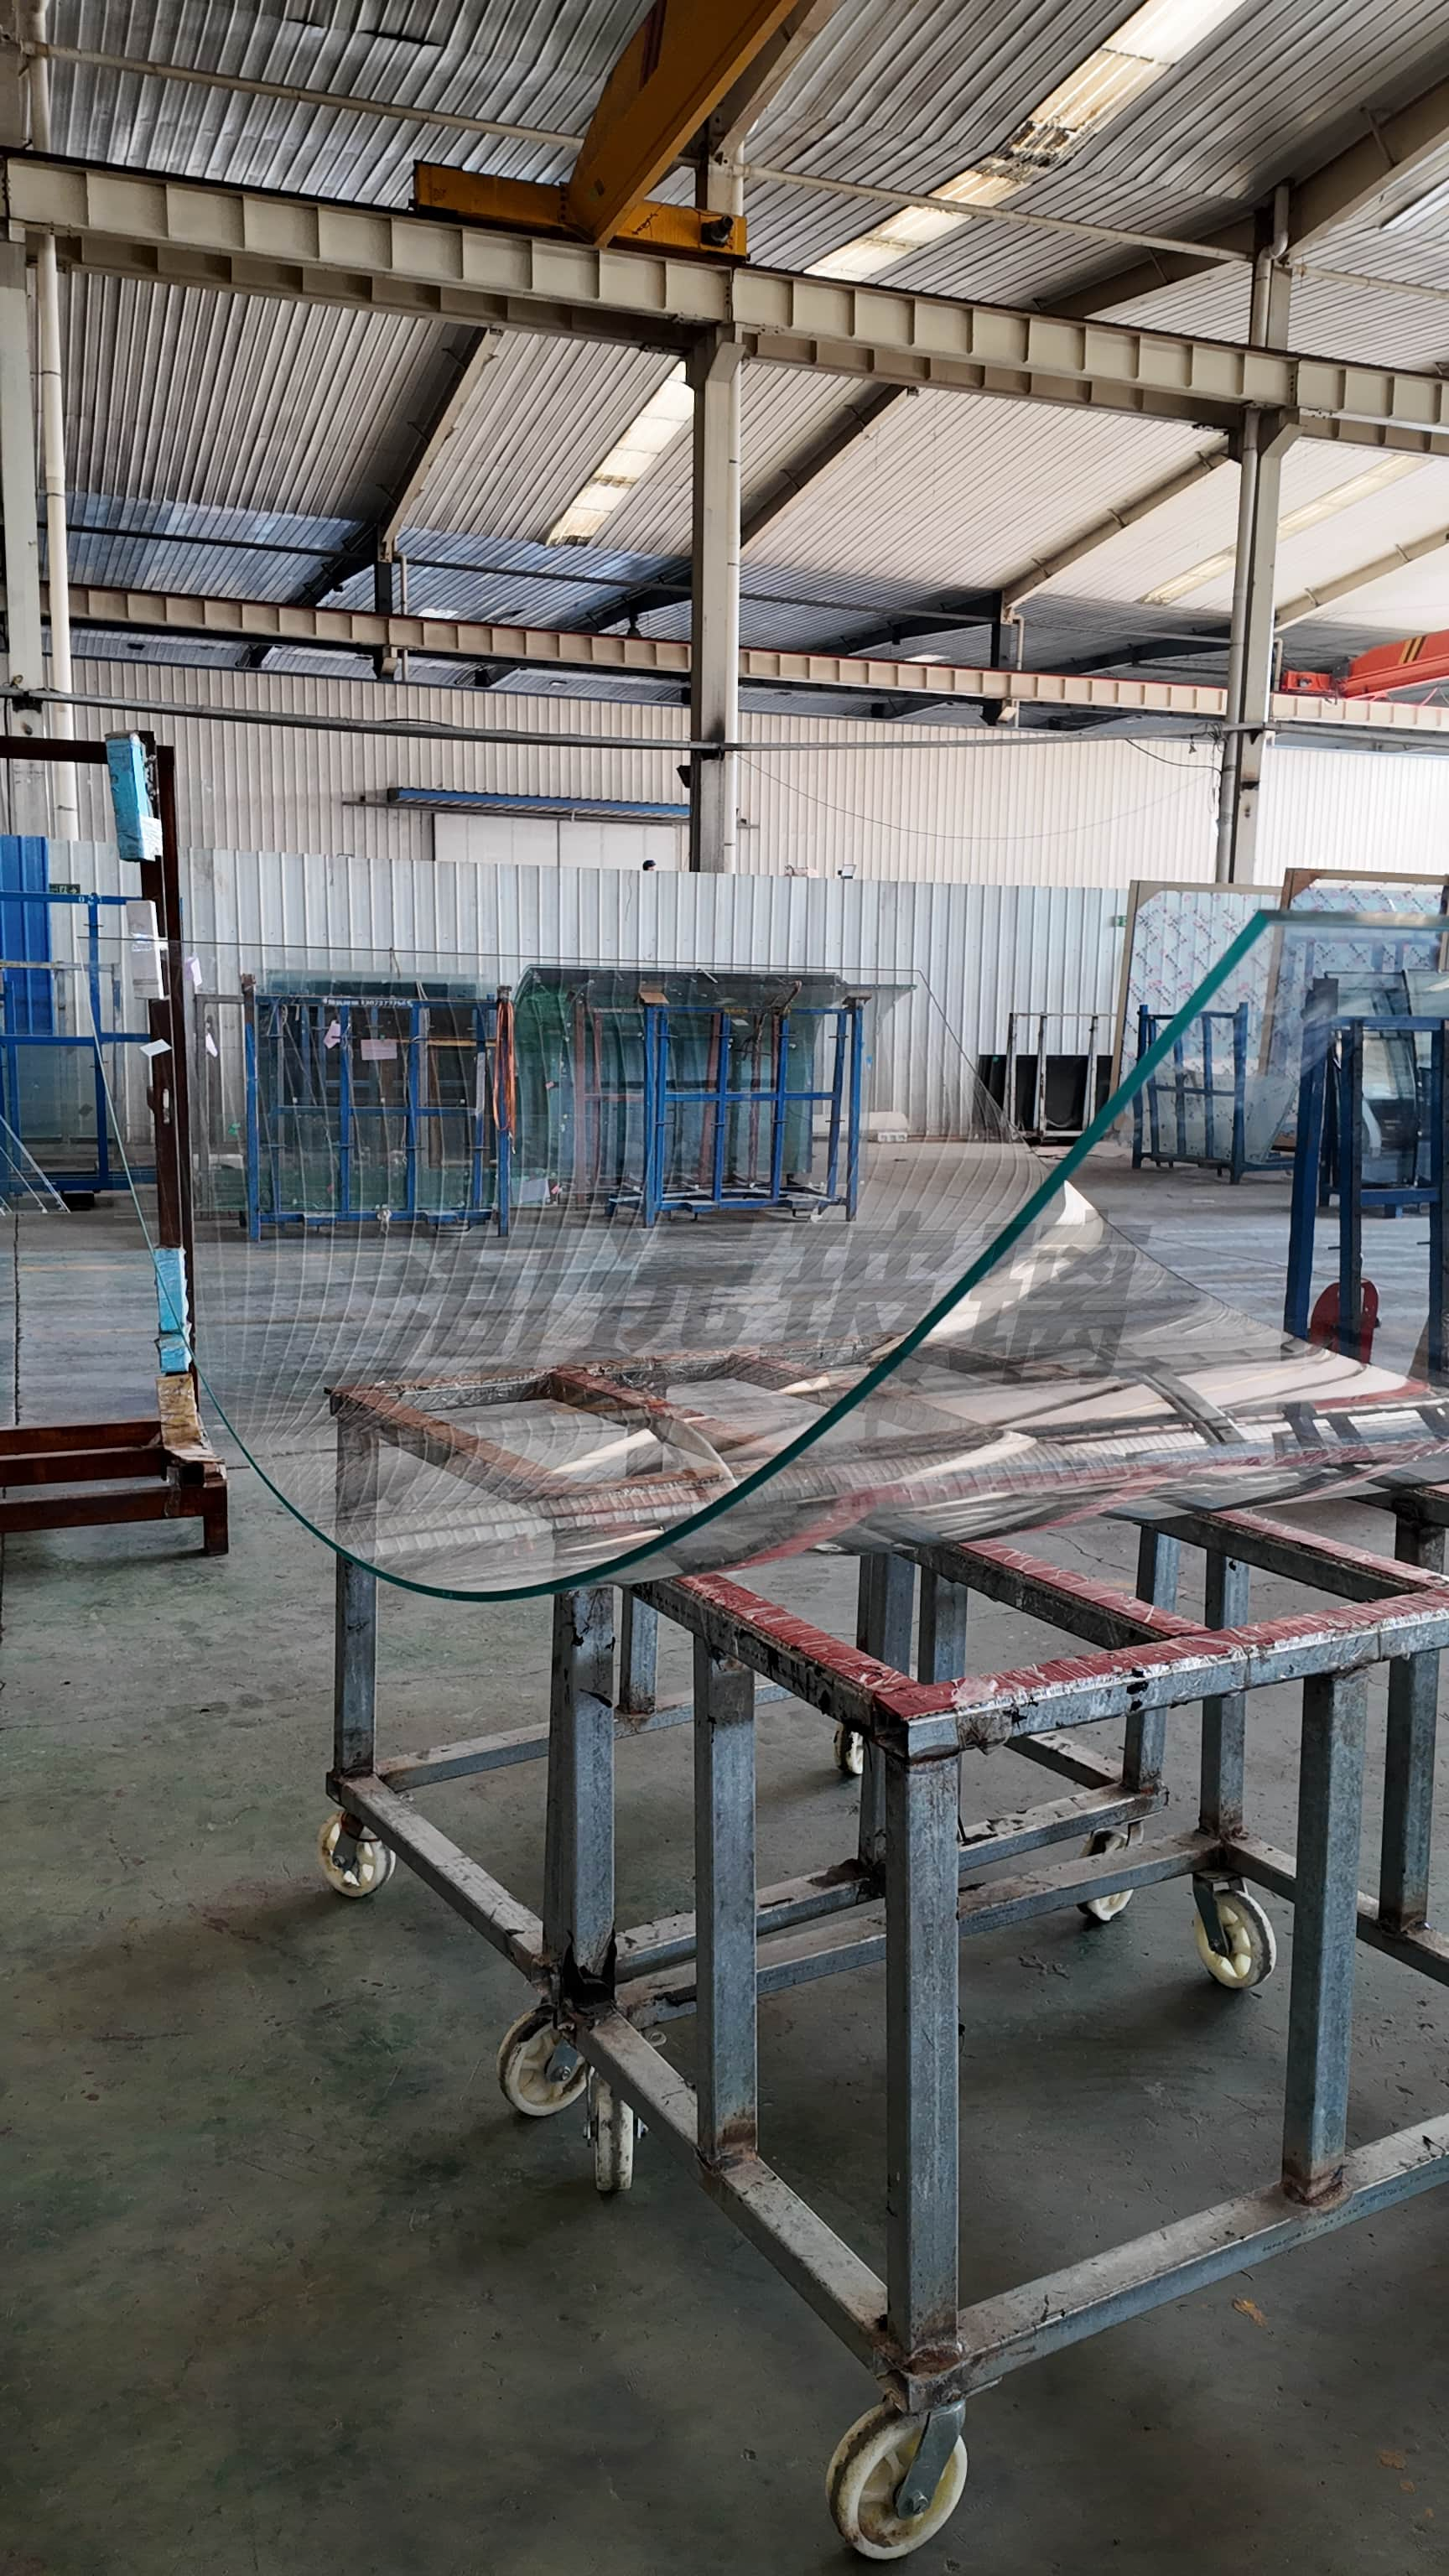
7.Thetwodefectsthatdominateonsite.Thefirstisbatchconsistency:panelsfromonebatchdonotfitthesamenodealike,andcrewsendupforcingthemintoplace.Ittracesbacktoforming—onedegreeoftemperatureorafractionofmouldoffsetchangestheresultingcurvature.Wereleaseabatchonlyafterfirst-pieceverification,sampleinprocessthroughouttherun,andkeeponemouldandoneparametersetperbatch.Thesecondappearsafterlaminationorinsulating:cornerliftandsealleakage.Twopanesmustmatchincurvaturebeforetheyareassembled;amismatchoffsetsthelaminationandunderminestheinsulatingseal.Wepairpanesfromthesamemouldandthesamebatch,verifycurvaturepairingbeforelamination,andre-setthelaminationcurveforeachorder'sactualcurvature.Edgesonsmall-radiuspartsalsoneedcontouredgingandchamfering,whichisharderthanonflatedges;everypanelischeckedagainstitsnumberbeforepacking.
8.Howtoscreenasupplier.**Cantheystateformingradiusandshaped-bendradiusinplainnumbers?Cantheyexplainthattoolingismadeforthespecificcurveratherthanreusingageneralmould?Doesthequotationitemisemouldandtrialcosts?Cantheynametheexactstagesatwhichfirst-pieceverificationandin-processsamplinghappen?Asupplierwhoanswersallfourclearlyremovesmostoftheuncertaintyfromyourprogramme.